
 EN
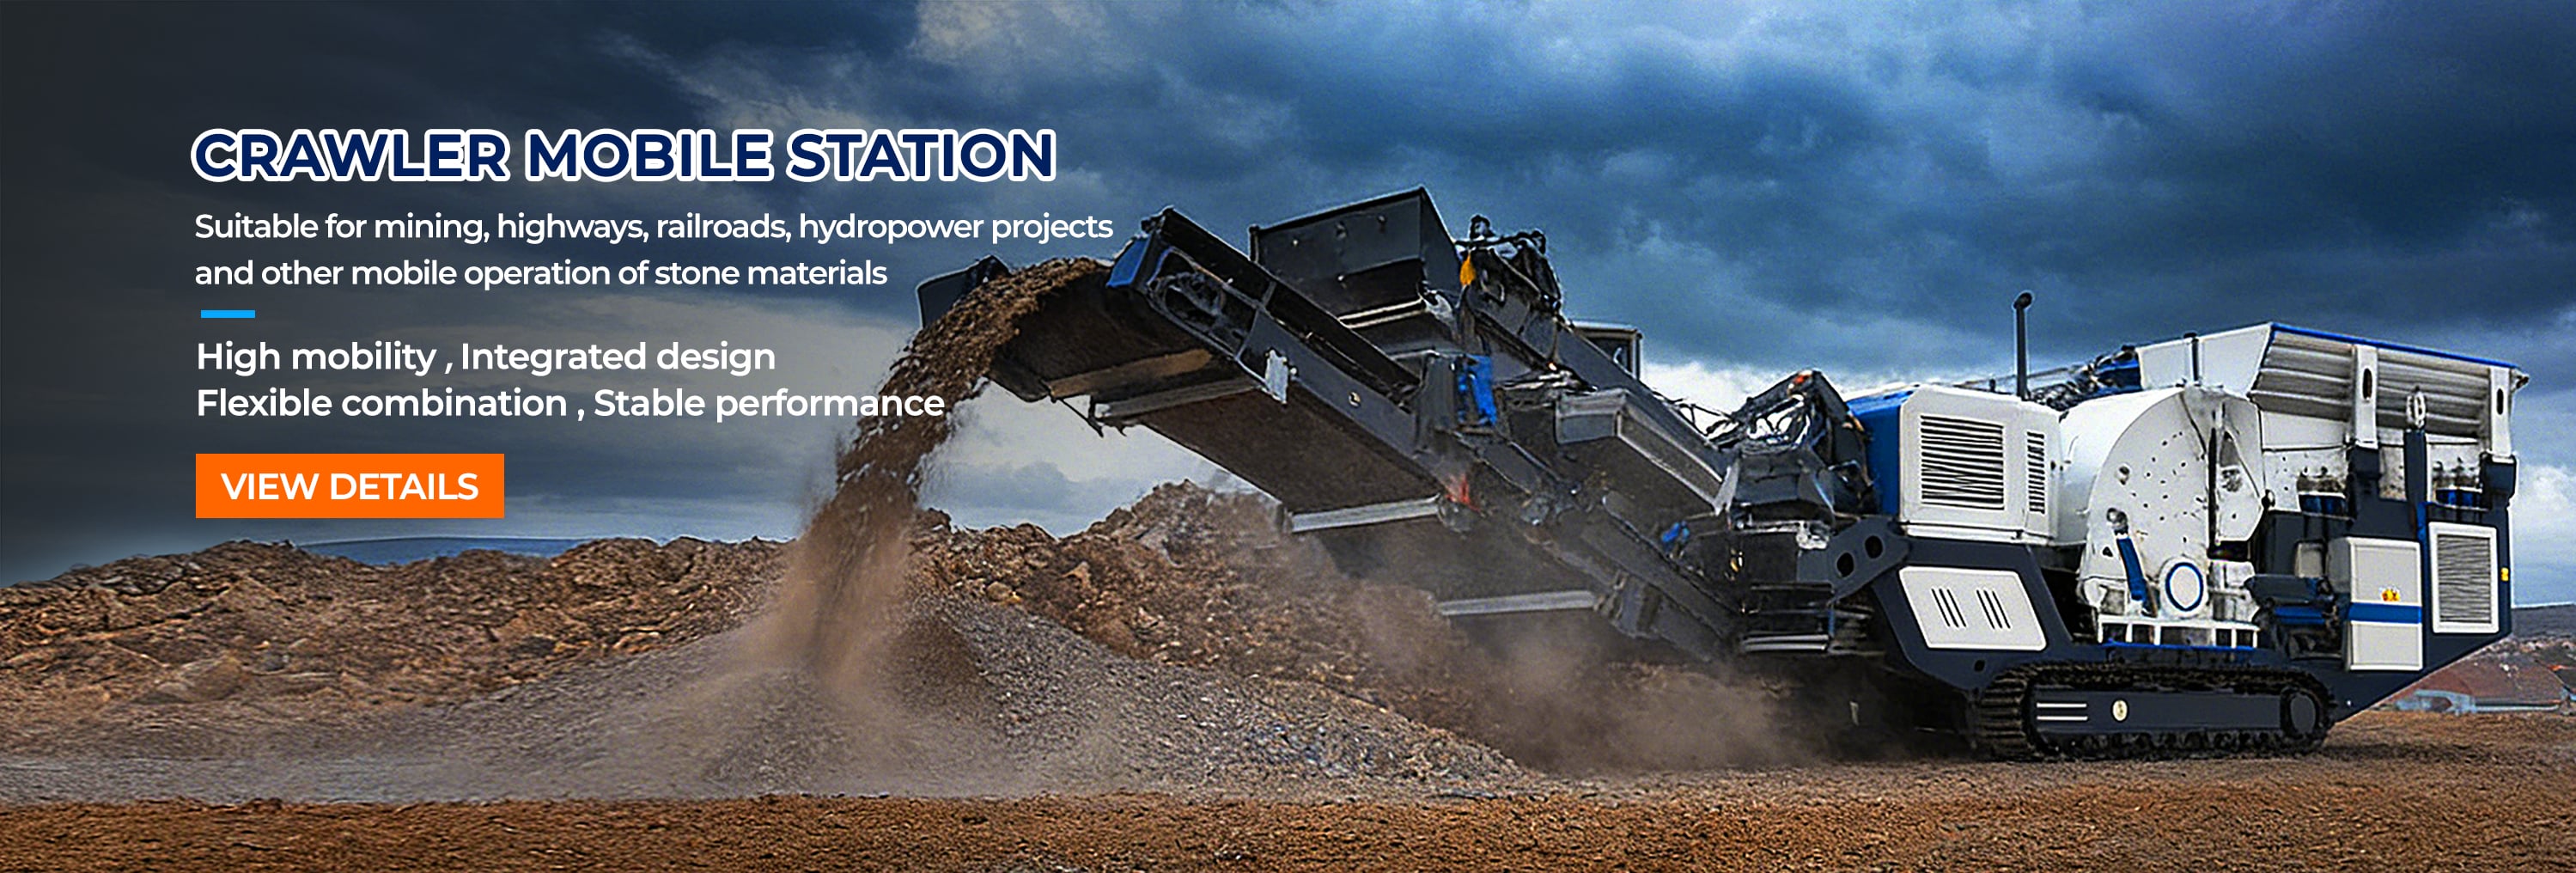
Modern aggregate operations live or die by tons-per-hour, and quarry crushing throughput is rarely limited by the crusher nameplate — it is limited by how the whole circuit is fed, screened, and maintained. Many sites already own capable equipment yet still lose output to avoidable bottlenecks. The following guidance focuses on the levers operators control every shift: feed-size discipline, gradation management, and planned downtime. The goal is clear — move more saleable aggregate through the same fixed assets without capital-heavy expansion.
Feed-Size Management Sets the Throughput Ceiling
Why Oversize Feed Chokes the Crushing Chamber
Quarry crushing chambers are designed around a target top-size, not a wish list. When boulders exceed the designed feed opening, the chamber bridges instead of fracture-compacting, and instantaneous motor load spikes while actual tons per hour collapse. The physics is straightforward: oversize rock occupies chamber volume without being reduced, starving the discharge belt of finished aggregate. A vibrating feeder with a grizzly section removes fines before the primary, protecting the chamber and stabilizing the reduction ratio. Material hardness and silica content also dictate how aggressively the chamber can be loaded. A site survey that maps feed-size distribution turns guesswork into a controllable variable.
Matching Feed Size to Reduction Ratio
For quarry crushing circuits, reduction ratio — the proportion of feed size to discharge size — decides how many crushing stages a production line needs. Pushing a single stage beyond its comfortable ratio forces recirculation and heat in the liner plate, accelerating wear parts consumption. A practical rule keeps primary reduction near 4:1 to 6:1 and relies on a secondary cone crusher or impact crusher for shaping. Zhongyu Dingli EPC teams routinely run a feasibility study before finalizing stage count, because over-reduction at one station steals throughput from the entire crushing plant. A modest reduction ratio margin at each stage reserves headroom for feed swings.
Gradation Control Through Screening Optimization
Screen Deck Selection and Aperture Strategy
In quarry crushing, the vibrating screen earns its place at the heart of productivity, because gradation is what the market actually buys. Deck number, aperture shape, and inclination set whether aggregate lands in a saleable size band or recirculates as waste. A 3YKQ multi-deck screen paired with correct mesh sizing keeps the particle size distribution tight, lifting the share of on-spec product without extra crushing energy. Operators should validate aperture wear monthly, because stretched meshes silently widen discharge size and dilute value. A well-tuned vibrating screen lowers conveyor load by sending only sized material downstream, keeping the belt scale honest.
Avoiding Recirculation Load Buildup
Effective quarry crushing minimizes recirculation, the silent thief of throughput. When screen undersize is mis-routed back to the crusher, the crushing plant processes the same rock twice, doubling energy per ton and crowding the crushing chamber. Closed-circuit balancing with a conveyor belt scale and a smart control system lets teams spot load creep early. Targeting a recirculation load under roughly 20 percent keeps motor power and operating cost in a healthy band while protecting spare parts inventory.
Downtime Reduction Through Maintenance Planning
Wear-Parts Strategy and Liner Monitoring
Across a quarry crushing plant, unplanned stops are the most expensive hours. Liner plate and rotor wear change the crushing chamber geometry, and a worn liner quietly drops throughput before it finally fails. A wear-parts program tracks thickness against tonnage, swapping components during planned windows rather than after a breakdown. Stocking the right spare parts on site and scheduling change-outs with commissioning data shortens the gap between failure detection and recovery. Conveyor belt alignment deserves equal attention, because a mistracking belt spills material and forces unscheduled stops.
Planned Shutdowns Versus Reactive Breakdowns
Reactive maintenance trades a cheap bearing for a lost production day. A planned shutdown bundles liner changes, belt checks, and dust control inspection into one controlled window, often aligned to OSHA and ANSI machine-guard expectations for safe access. NFPA guidance on dust systems matters where silica content is high, since combustible fines demand disciplined housekeeping. The payback period on a maintenance calendar is usually recovered in a single avoided breakdown, protecting both output and crew.
Proven Results From a Modular Granite Quarry Line
Background and the Productivity Gap
This scenario reflects a real modular granite line built for a client in Timor-Leste, where a 50–500 TPH modular steel-structure design replaced a slower traditional build. The background was a remote site, a tight labor pool, and a need for fast ramp-up. The problem faced was low initial uptime — manual assembly and weak feed-size control throttled aggregate output well below the design tons per hour. Traditional concrete foundations would have extended that productivity gap for months.
Solution Adopted and Measurable Effect
The solution adopted was a prefabricated, containerizable modular design with on-site assembly and an integrated smart control system for feed and screening, delivered under an ISO 9001 quality framework. Measurable effect: installation time dropped by roughly 50 percent and labor by about 40 percent versus a traditional build, letting the production line reach target throughput far sooner. With disciplined feed-size management and gradation control, the circuit now sustains quarry crushing productivity across the 50–500 TPH range. The case shows that throughput gains come as much from layout and control as from the crusher itself.
Maximizing output is less about buying bigger machines and more about running the existing circuit tighter. Feed-size discipline protects the crushing chamber, gradation control lifts the share of saleable aggregate, and planned maintenance converts lost hours into steady tons per hour. For operations evaluating a new line, a site survey and feasibility study frame the real opportunity before capital expenditure is committed. Effective quarry crushing is an operating discipline first and a hardware choice second — the discipline is what compounds into high productivity.
Frequently Asked Questions
Question
What feed-size limit protects throughput in a crushing circuit?
Answer: Oversize feed above the chamber opening causes bridging and collapses tons per hour. Keep top-size at or below the designed feed opening and pre-screen fines with a grizzly vibrating feeder. A site survey mapping the size distribution identifies the real ceiling. Controlling feed size is the most cost-effective throughput lever, because it protects the crushing chamber and stabilizes the reduction ratio without new capital.
Question
How does a vibrating screen improve aggregate gradation?
Answer: A multi-deck vibrating screen separates material into tight size bands, lifting the share of on-spec product. Correct aperture shape and inclination reduce mis-routed fines that otherwise recirculate. Effective quarry crushing depends on pairing the screen with disciplined feed so the circuit makes saleable aggregate the first pass. Monthly mesh checks prevent stretched openings from silently widening discharge size and lowering product value.
Question
Why does planned maintenance beat reactive repair?
Answer: Reactive breakdowns trade a cheap component for a lost production day. A planned shutdown bundles liner changes, belt checks, and dust inspection into one controlled window. Tracking wear-parts thickness against tonnage schedules swaps before failure, shortening recovery time. Aligning work to OSHA and ANSI access standards also improves safety. The payback period on a maintenance calendar is often recovered in a single avoided stoppage.
Question
Can smart control systems raise tons per hour?
Answer: Yes. A smart control system reads conveyor belt scales and screen load, then adjusts feeder speed and apertures to keep the circuit balanced. Early detection of recirculation creep prevents the crushing chamber from crowding, sustaining steady throughput. Remote monitoring also shortens response when gradation drifts. While no technology replaces good feed discipline, digital control converts small losses across a shift into measurable daily gains.
Question
Which standards guide safe quarry and dust practice?
Answer: OSHA and ANSI cover worker safety and machine guards for crushing equipment access. NFPA guidance applies where combustible dust and high silica content create explosion or health risk, demanding disciplined housekeeping. ISO 9001 supports consistent quality management across the production line. Following these frameworks reduces incident exposure and keeps the plant available. Specifying compliance during procurement protects both crew and operating continuity.