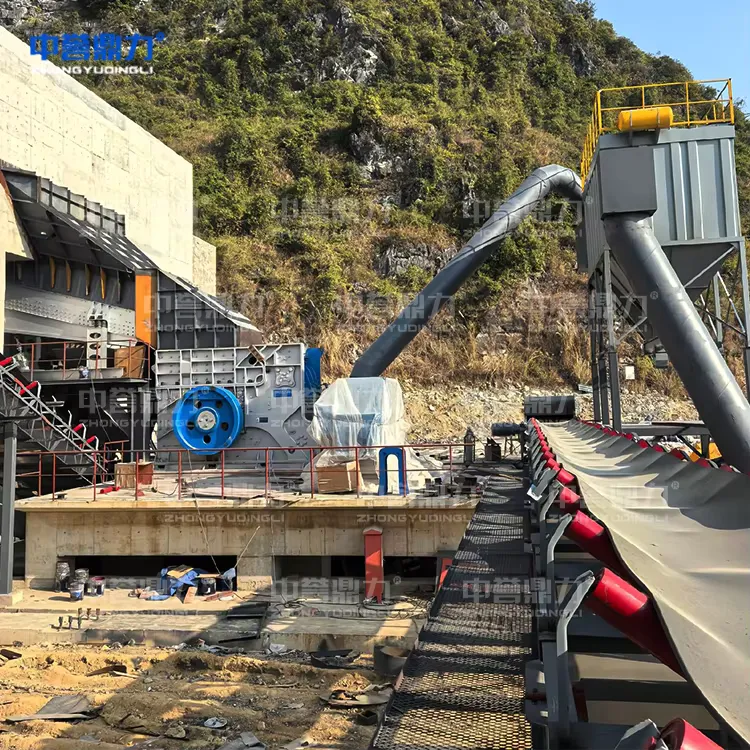
The Shaker Feeder plays a crucial role in material handling systems across multiple industries, including mining, construction, and aggregate processing. Its primary function is to regulate the flow of bulk materials into crushers, screens, and other processing equipment. By utilizing a combination of vibration and gravity, the Shaker Feeder efficiently moves materials while minimizing the risk of blockages and ensuring a consistent feed rate. This capability is essential for maintaining optimal production levels and enhancing the overall efficiency of the operation. Zhongyu Dingli’s Shaker Feeders are designed with advanced technology that allows for easy adjustments to vibration intensity and feed rates. This flexibility enables operators to customize the equipment based on the specific characteristics of the materials being handled, whether they are coarse aggregates, fine powders, or other bulk materials. Additionally, our Shaker Feeders are built with robust materials, ensuring long-lasting performance even in harsh environments. Moreover, the integration of intelligent solutions into our Shaker Feeders enhances their functionality. For instance, real-time monitoring systems can be incorporated to track performance metrics, allowing for proactive maintenance and minimizing downtime. This level of innovation is part of Zhongyu Dingli’s commitment to providing comprehensive solutions that prioritize efficiency, reliability, and sustainability in material handling. In conclusion, the Shaker Feeder is an indispensable asset for any operation looking to optimize its material handling processes. With Zhongyu Dingli’s expertise and commitment to quality, you can trust that our Shaker Feeders will deliver the performance and reliability you need to succeed in today’s competitive market.